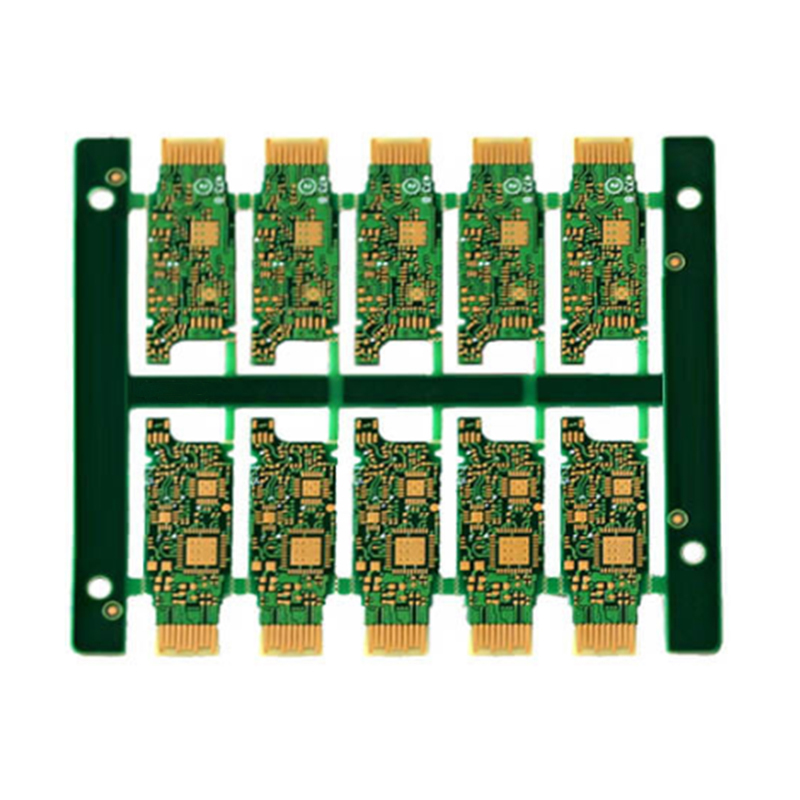
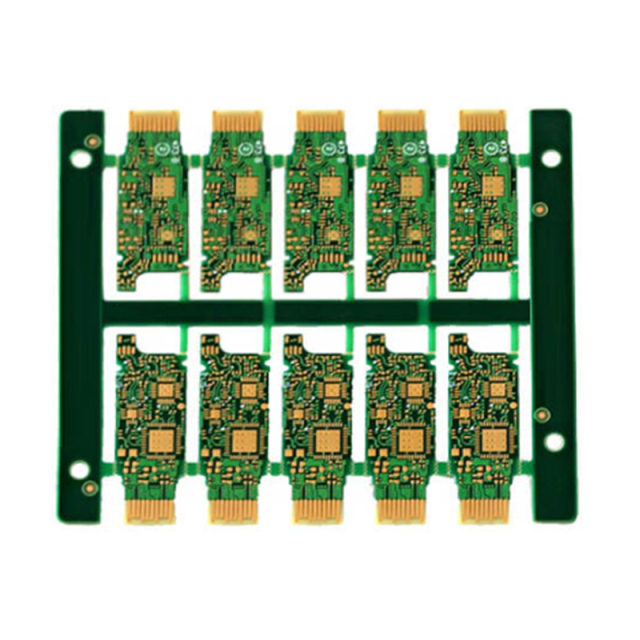
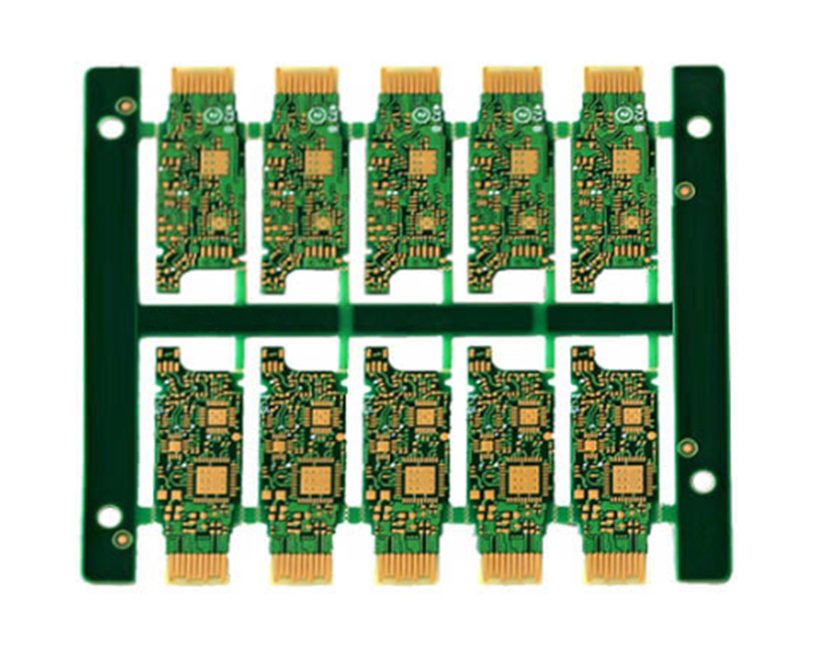
Product Model: Optical Module HDI PCB Layer Quantity: 8 Layers Substrate Material: FR4, High‑Tg 170℃ HDI Configuration: 2+4+2 stack‑up HDI structure Board Finished Thickness: 0.8 mm Copper Foil Thickness: 0.5 oz Solder Mask Color: Green / White (optional) Surface Finish Process: Electrolytic Hard Gold Special Manufacturing Technology: Gold finger beveling design Minimum Trace Width / Spacing: 3 mil / 3 mil
This HDI PCB board is built for the inside of an optical transceiver, where a few square centimetres of laminate have to carry high-speed differential pairs, sit inside a machined metal housing and survive repeated plugging into a cage. The stack-up is 2+4+2 across eight layers: two high-density outer layers carry the fine routing, a four-layer core handles power and ground, and the HDI layers reach the pins that cannot be routed on the surface. The finished board is thin and stiff enough for a compact module shell, and its outline is tight enough that every millimetre has a job to do.
Most customers arrive with the housing already drawn and the link budget already simulated, so the board has to meet their mechanical and electrical targets rather than the other way round. We fabricate to your drawing and stack-up, and this board sits alongside the other PCB solutions we supply for optical communication hardware: high-speed laminate boards, gold finger PCB fabrication and the assembly work that follows them.
| Model | Optical Module HDI PCB |
|---|---|
| Layer count | 8 |
| Stack-up | 2+4+2 HDI |
| Base material | FR-4, high-Tg 170 °C |
| High-speed material options | Rogers series, Panasonic M6 |
| Finished board thickness | 0.8 mm |
| Copper foil thickness | 0.5 oz |
| Minimum trace / spacing | 3 mil / 3 mil |
| Solder mask | Green / white (optional) |
| Surface finish | Electrolytic hard gold |
| Gold finger design | Staggered long-short fingers, bevelled edge |
| Board area | 3–5 cm² |
| Outline tolerance | Class 3 |
| Application | Optical module transceiver board |
An optical module is built from three groups of parts: the optoelectronic devices, the functional circuit modules and the optical interfaces. The optoelectronic side splits again into a transmitting assembly, which turns electrical signals into light, and a receiving assembly, which turns light back into electrical signals. The board sits in the middle of that chain. It carries the circuitry between the optical sub-assemblies and the host, and hands the signal to the gold-finger edge connector that plugs into the cage — which is why the outline, the finger length and the via structure matter as much as the layer count.
Because the board is one element of a wider assembly, most programmes hand it to a PCB assembly manufacturer and build it into the module through a custom assembly flow rather than treating it as a stand-alone part. That changes what the board has to survive: reflow alongside the optical sub-assemblies, handling between stations, and a final power-up test where the link is measured. If your line does that work, tell us early — panel layout and mask openings are settled at fabrication, not afterwards.
5G construction is expected to drive demand for close to 250 million core-kilometres of optical cable. That number is a forecast rather than a schedule: the bearer deployment scheme is still open in places, and both the C-RAN split ratio and the take-up of WDM equipment in the fronthaul move the figure. Under the 5G SA architecture, fibre is needed in the fronthaul, the backhaul and the bearer network at the same time, and projected consumption could exceed market expectations by around 100 million core-kilometres — a marginal lift for the whole optical communication chain rather than a step change.
For anyone specifying the board, the practical reading is that module volume will keep shifting between fronthaul and midhaul as operators settle their splits. A high-speed PCB stack-up that can be re-tuned for a different port count is worth more over the life of a programme than one optimised for a single forecast.
Boards leave us panelised with routed breakaway rails, which is what keeps a thin core flat as it travels through solder-paste printing and placement. Snap them out at the rail rather than flexing the board, and keep the panel supported on a flat surface while you do it — a thin HDI board bends further than a standard 1.6 mm board before it cracks. The gold fingers are the other fragile point: leave the protective tape in place until the module is mated, handle the board by its edges and keep bare hands off the gold. Skin oils and stray solder paste are the usual reasons a plated finger turns intermittent after a few insertion cycles. The bevel on the leading edge is there to guide the board into the cage, so if insertion feels tight, check the housing chamfer before you change anything on the board. And if the panel goes straight onto your own PCB assembly services line, tell us the conveyor width and rail depth before we route it, so the rail is not trimmed off at your end.
Maxipcb builds high-reliability circuit boards for the electronics industry. The PCB solutions we produce most often are multilayer boards, prototype boards, high-speed boards, high-frequency boards, gold finger boards, gold-plated boards, impedance control boards, ceramic circuit boards and fine-pitch boards. This optical module board draws on three of those lines at once: fine-pitch etching, gold finger finishing and high-speed laminate.
Because the same plant also runs PCB assembly services, a programme that starts as a bare board can later be supplied populated without the drawing moving to a second supplier. One set of files, one stack-up record and one point of contact stay with the project from the prototype panel through the production batch.
As a PCB assembly manufacturer we work from customer drawings rather than from a catalogue, which is why the questions we ask before quoting concern your housing, your cage and your loss budget rather than a part number. If a design needs a stack-up we cannot hold reliably, we would rather say so before the order than after it.
On this gold finger PCB, the fingers are a contact surface, not a solder joint, and the finish is chosen for that job rather than borrowed from the component side. The edge connector is plated with electrolytic hard gold over a nickel barrier; the alloyed gold deposit is hard enough to take repeated insertion and withdrawal in a cage without smearing or thinning at the leading edge. The bevel on the finger tips is cut at the same stage, so the plated surface runs continuously over the chamfer instead of ending in a bare laminate edge that would catch inside the connector shell.
A solderable finish would be the wrong choice for this area. Immersion gold, OSP and HASL are specified for wetting — they exist so paste or wave solder forms a proper joint, and the gold in an immersion deposit is deliberately thin. On an edge connector that thin layer wears through after a limited number of mating cycles and exposes the nickel underneath, which pushes contact resistance up and turns a link intermittent. Electrolytic hard gold carries the thickness and the hardness to stay intact for the working life of the module, which is why we do not substitute an immersion finish on the fingers even when the rest of the board uses one.
Many optical module boards need both finishes at once. Pads that receive components still need a solderable surface and open solder mask windows; the finger area needs hard gold and stays mask-free. We define those two areas on the fabrication drawing and finish each to its own requirement, so the connector does not have to be compromised to keep the assembly solderable. Mark the contact area and the solder area on the drawing you send, and we will confirm the finish split with you before the production panel is tooled.

Maxipcb is a printed circuit board manufacturer with more than ten years of production history. We take on custom work from prototype samples through small-batch and volume orders, so buyers deal with a single factory rather than a chain of subcontractors. OEM manufacture is available for customers who need boards built to their own specifications. A full-process quality system — incoming, in-process and outgoing checks — runs on every job, and customer designs and process files stay confidential.
The numbers describe how the eight layers are grouped. Two HDI layers sit on each outer face with a four-layer core in the middle, so 2 + 4 + 2 = 8. The outer HDI layers carry the 3 mil / 3 mil routing and the blind vias that drop to the first inner layer, while the core handles power, ground and slower signals. That is what lets an HDI PCB board this small escape a high pin-count package without growing its outline.
Long-short, or staggered, fingers make the module mate in a set order. The longer fingers — ground and power — reach the host connector first, so the module is referenced before any signal pin connects, and the shorter signal fingers make contact last. The bevel on the leading edge guides the board into the cage and stops a finger catching on the connector shell. Both details are decided at fabrication, so the finger lengths need to be on the drawing.
The standard product is the bare HDI board, built to your stack-up and outline. Where a programme also needs the board populated, custom PCB assembly covers SMT and through-hole work from the same drawing set, using components we source or parts you supply. Send the BOM together with the fabrication drawing and the two can be quoted and built as one project.
Yes — the prototype is not a different process. It uses the same stack-up, the same Class 3 outline control and the same electrolytic hard gold, just on a smaller panel. Our PCB prototype service exists so the first boards can go into the housing and the cage for fit and insertion checks before a production panel is committed. Keeping both stages on one process is what makes the prototype result meaningful for the volume build.
Yes. Beyond this board, the PCB solutions we supply for module work include high-frequency boards, high-speed boards, gold finger boards, impedance control boards, rigid-flex and IC substrates. A module programme often needs a main board, a small interconnect and a test fixture board at the same time, and it helps to have them built to one set of tolerances and one documentation set.
The fingers are a contact surface, not a solder joint. Hard gold is chosen for wear resistance: it holds up to repeated insertion and withdrawal in a cage, where a thin immersion finish would wear through to the nickel underneath and push contact resistance up. Solderable finishes belong on the pads where components are attached, not on an edge connector that has to survive repeated mating.
Model : Optical Module HDI PCB
Layers : 8Layers
Material : TG170 FR4
Construction : 2+4+2 HDI PCB
Finished Thickness:0.8mm
Copper Thickness : 0.5OZ
Color : Green/White
Surface treatment: Electric hard gold
Special technology: golden finger bevel
Min Trace / Space:3mil/3mil
Application : Optical Module HDI PCB